Surface Finishes / Plastic Injection Finishes
Plastic Injection Finishes
SPI polish grades, mold textures, painting and marking for injection-molded housings and visible consumer parts.
Get a Quote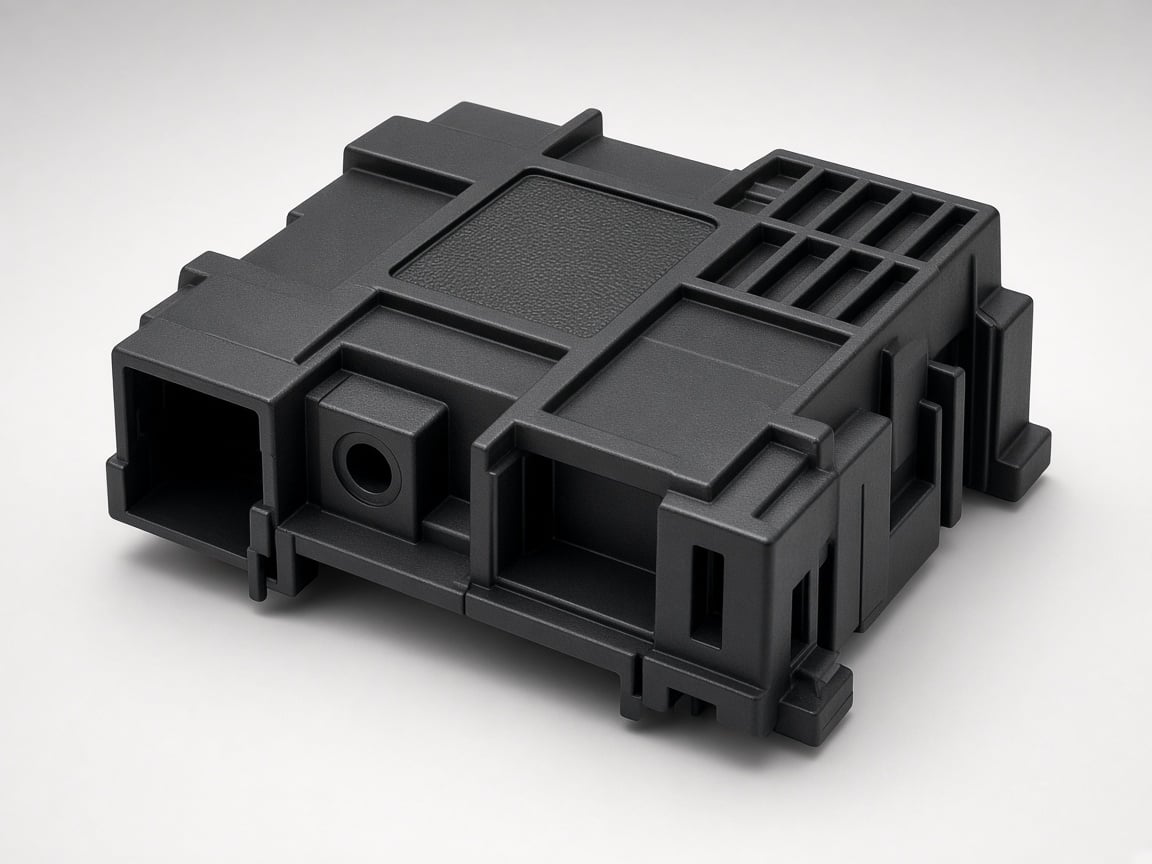
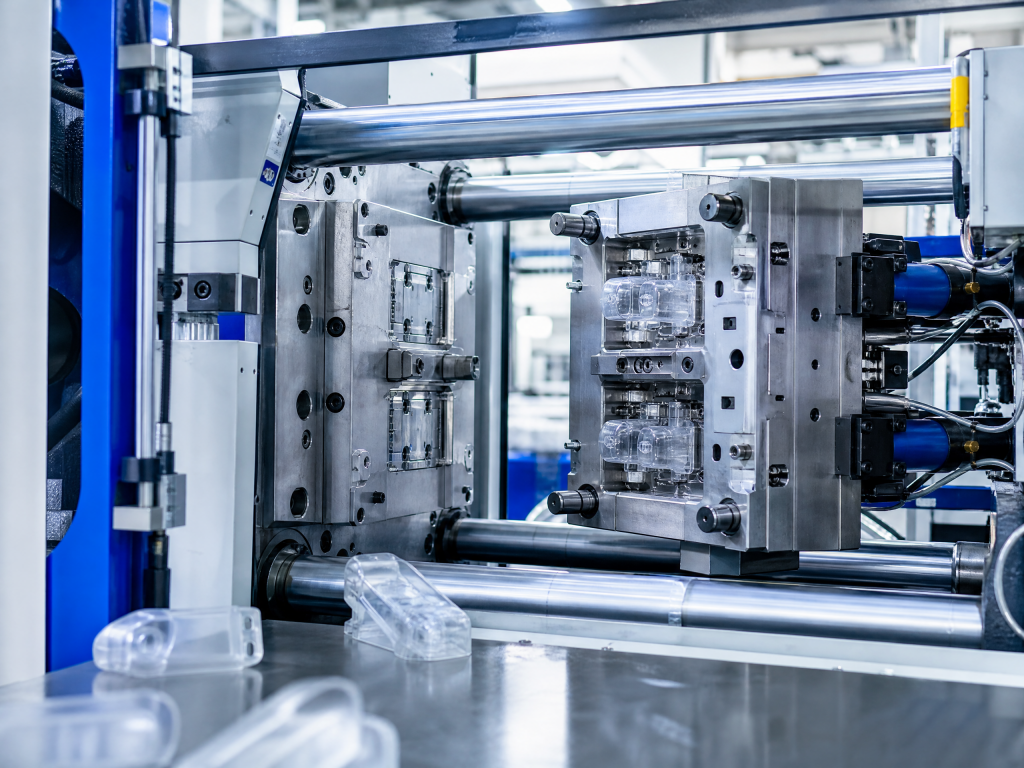
Plastic injection finishes start in the mold. SPI polish and texture decide most of the visible surface; painting, soft-touch coating and marking come after molding when color or branding goes beyond the resin. Stick Industry aligns tool finish with secondary processes so cosmetic parts stay repeatable in volume.
In-mold surface for injection parts
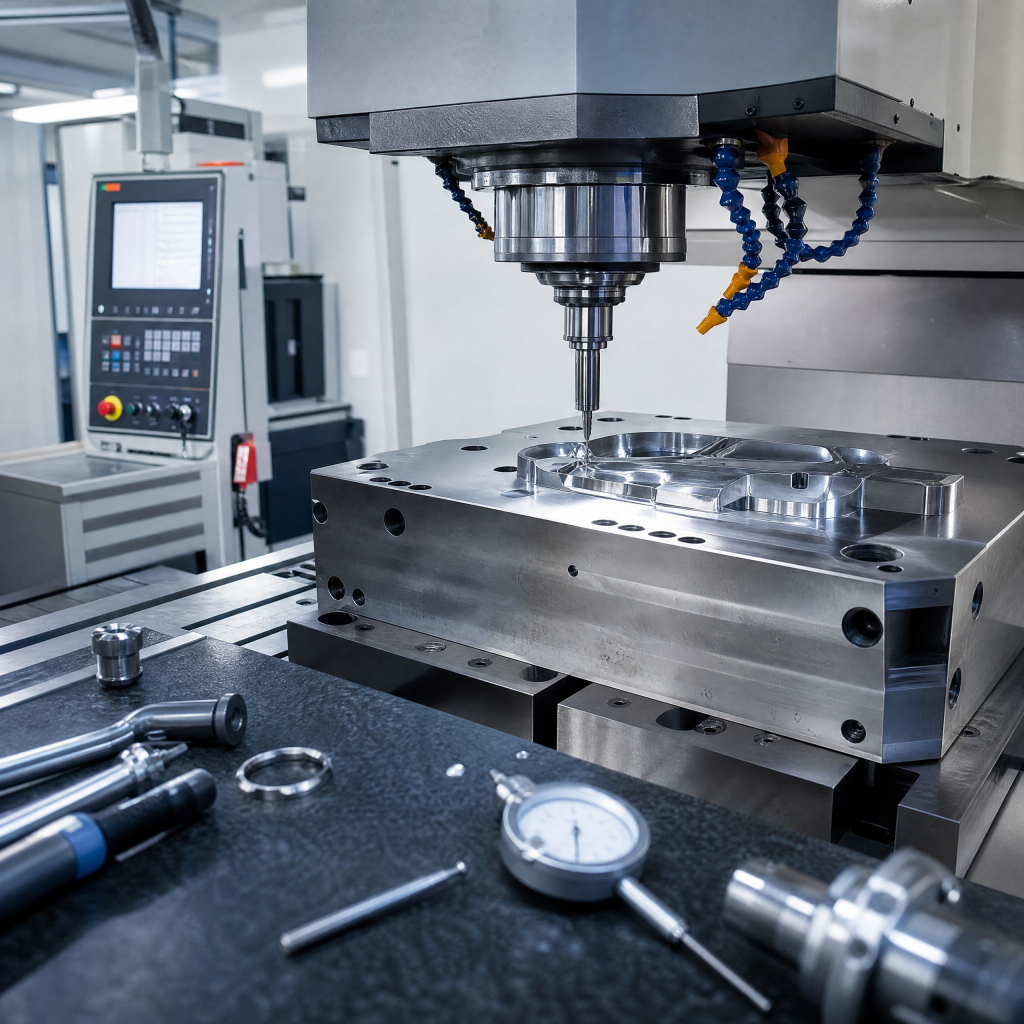
Tool steel polish and etch set gloss, texture and knit-line visibility before the first shot. Gate and ejector layout should keep marks off A-surfaces or under labels.
- SPI / SPE polish — A1–A3 high gloss, B for general cosmetics, C/D for non-visible faces
- Texture — MT / VDI / custom etch for grip or OEM match
- Gate & ejector plan — marks kept off cosmetic faces
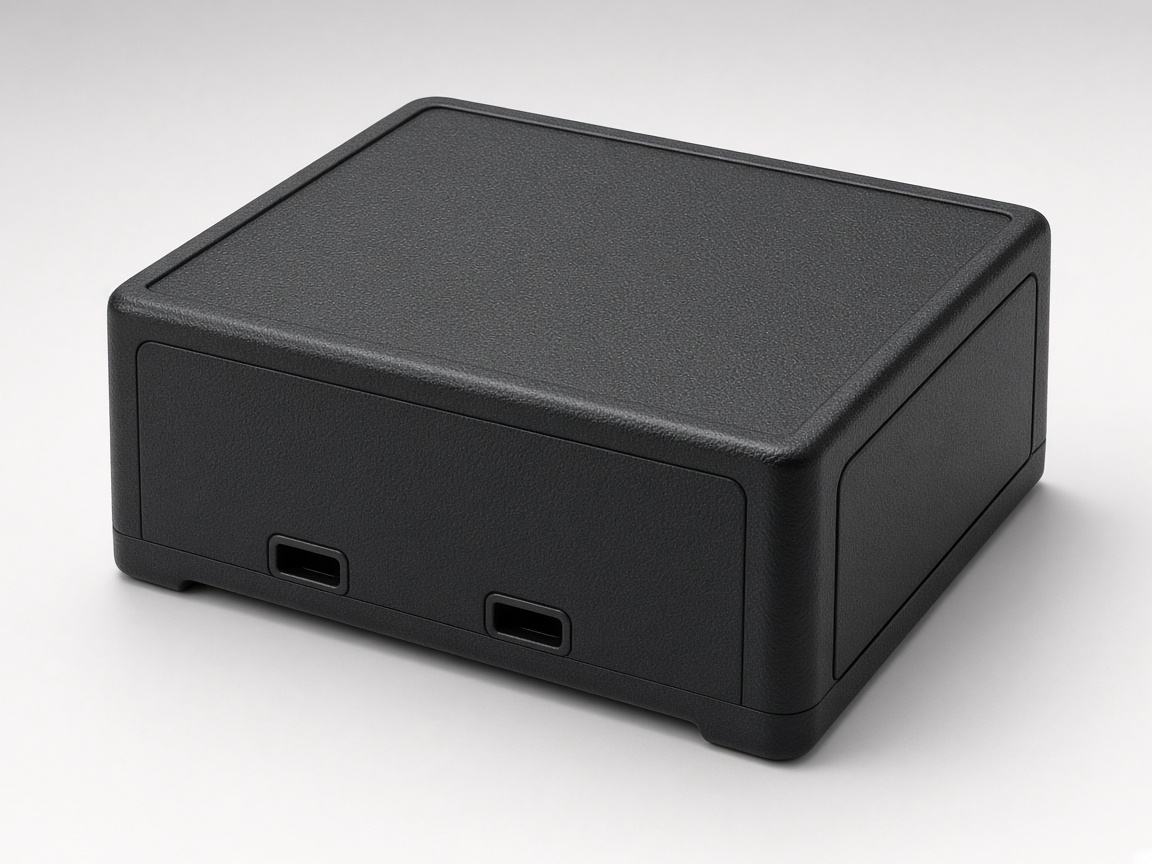
Secondary finishing after molding
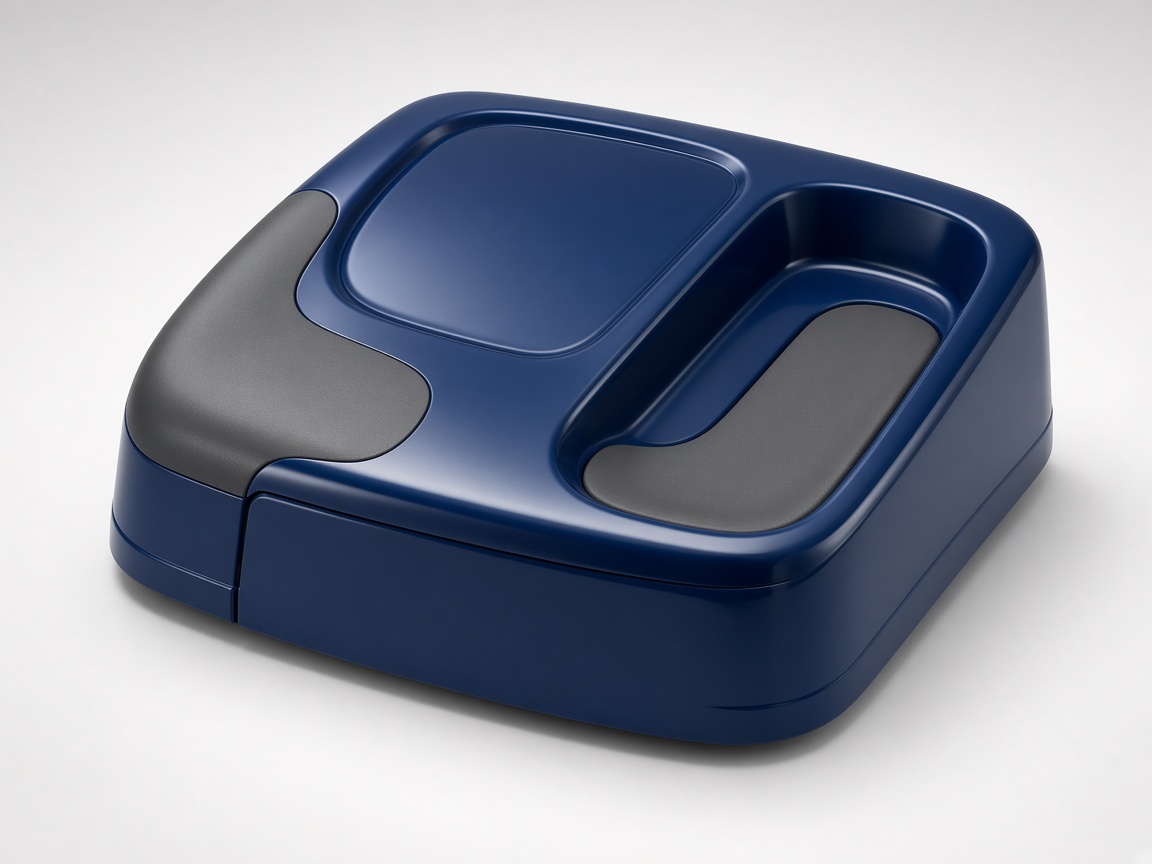
When resin color alone is not enough, we arrange spray painting, soft-touch coating, pad printing, silk screen, laser marking and EMI coating. Paint and soft-touch need mold finish that holds adhesion; we avoid over-polishing faces that will be painted later.
What to send for a finish quote
List resin grade, color target, SPI or texture code, and which faces are cosmetic. If painting or printing is planned, note mask areas and logo artwork early. Matching mold polish to paint saves cost and avoids rework when the tool is already cut.
We support DFM reviews for visible parts so sink, weld lines and ejector marks are handled before steel is hardened.
Full custom manufacturing services: prototypes & mass production with precise CNC, injection molding, sheet metal and 3D printing solutions.